Projects
Case studies from the shop floor.
Furnaces we've diagnosed, rebuilt and electrified, and what changed on each.
How we work
From first visit to a furnace back in production.
One team at every step, answerable for the result.
Step 01
Listen
Your process, your parts and what the furnace is doing wrong, in your own words.
Step 02
Assess
On site: atmosphere, heat loss, uniformity and controls, measured rather than assumed.
Step 03
Design & specify
The fix engineered for your process, with every component specified.
Step 04
Build & install
The fix built and installed to the design, with the site work managed end to end.
Step 05
Commission & validate
Calibration, trials and a uniformity survey before the furnace goes back to production.
Step 06
Stay with it
Maintenance, spares and support for the life of the furnace.
6 projects
 Retrofit
Pit furnace
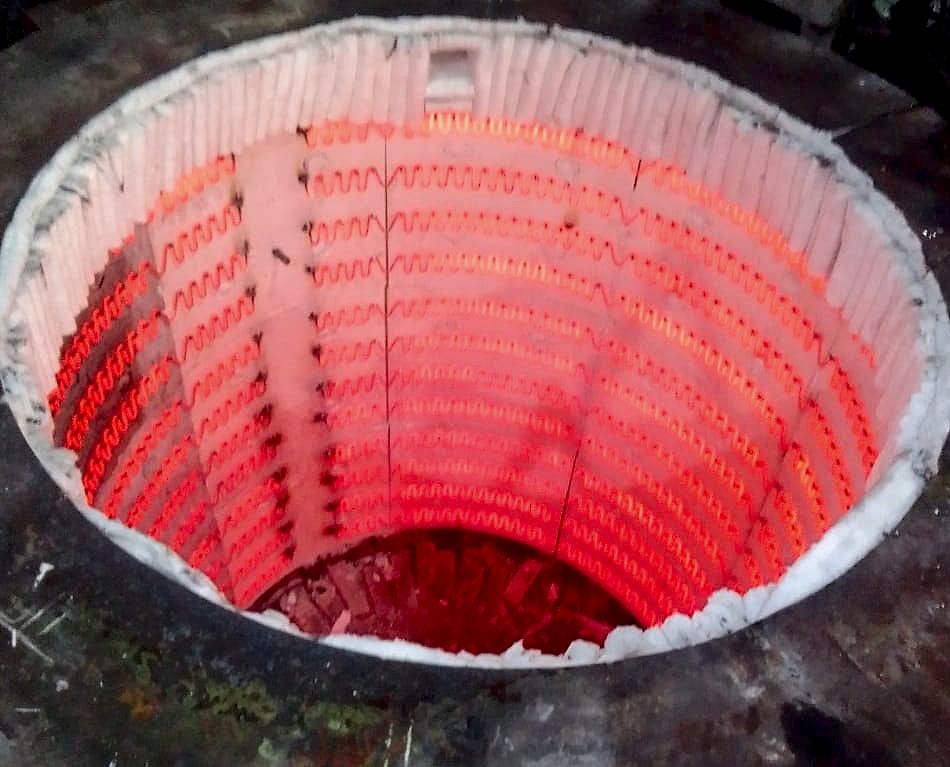
Retrofitting a pit furnace using a Fibrothal based heating system
An automotive components manufacturer's pit furnace re-lined with a Fibrothal heating system and ROB elements designed for line voltage, so the power transformer and its losses could go.
- Per batch
- 1,200 kg
- Rated power
- 115 kW
 Retrofit
Sealed quench furnace
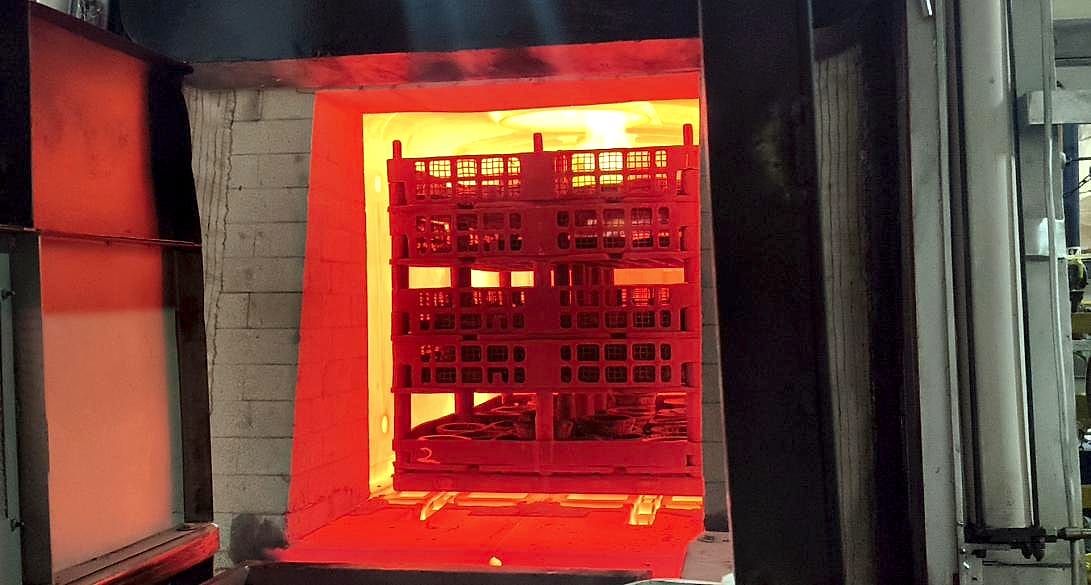
Bringing a sealed quench furnace back into production
A bearing manufacturer's sealed quench furnace was not in working condition. We rebuilt it across eight workstreams and handed it back to production in January 2026.
- Workstreams in one revamp
- 8
- Quench-oil level sensors
- 2 → 4
 Electrification
Sealed quench furnace
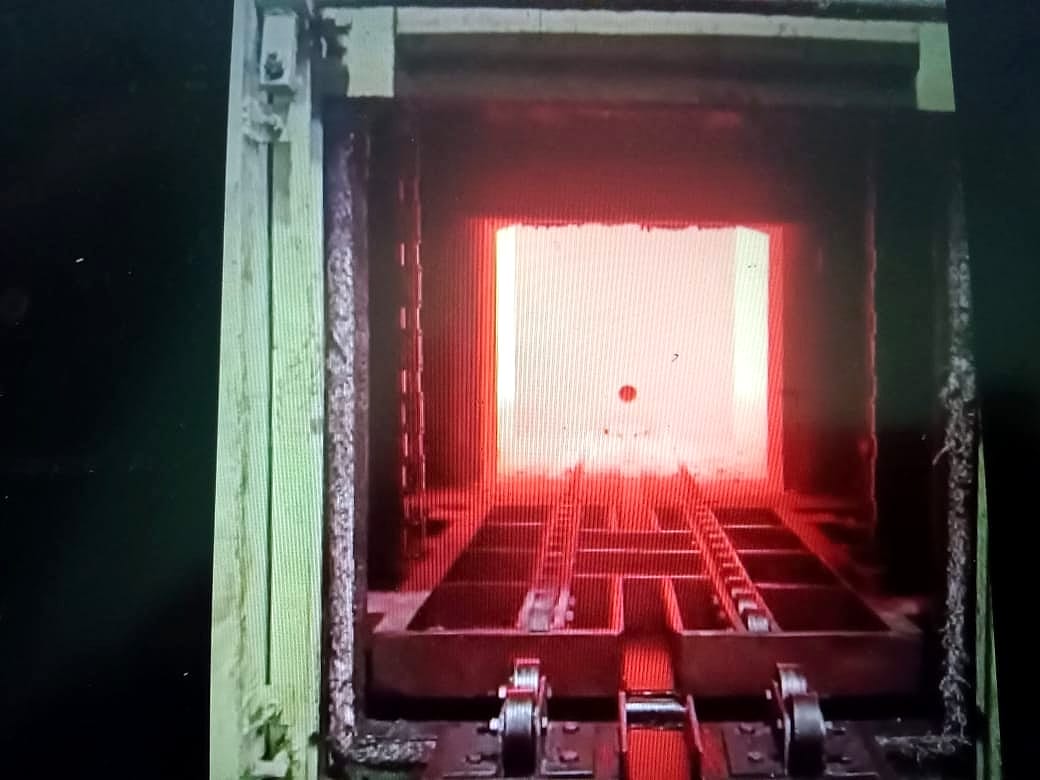
Converting a gas-fired sealed quench furnace to electric heating
A gear manufacturer's gas-fired sealed quench furnace converted to electric heating, with elements in radiant tubes and thyristor control, running at 920–980 °C.
- Operating temperature
- 920–980 °C
 New furnace
Bell furnace
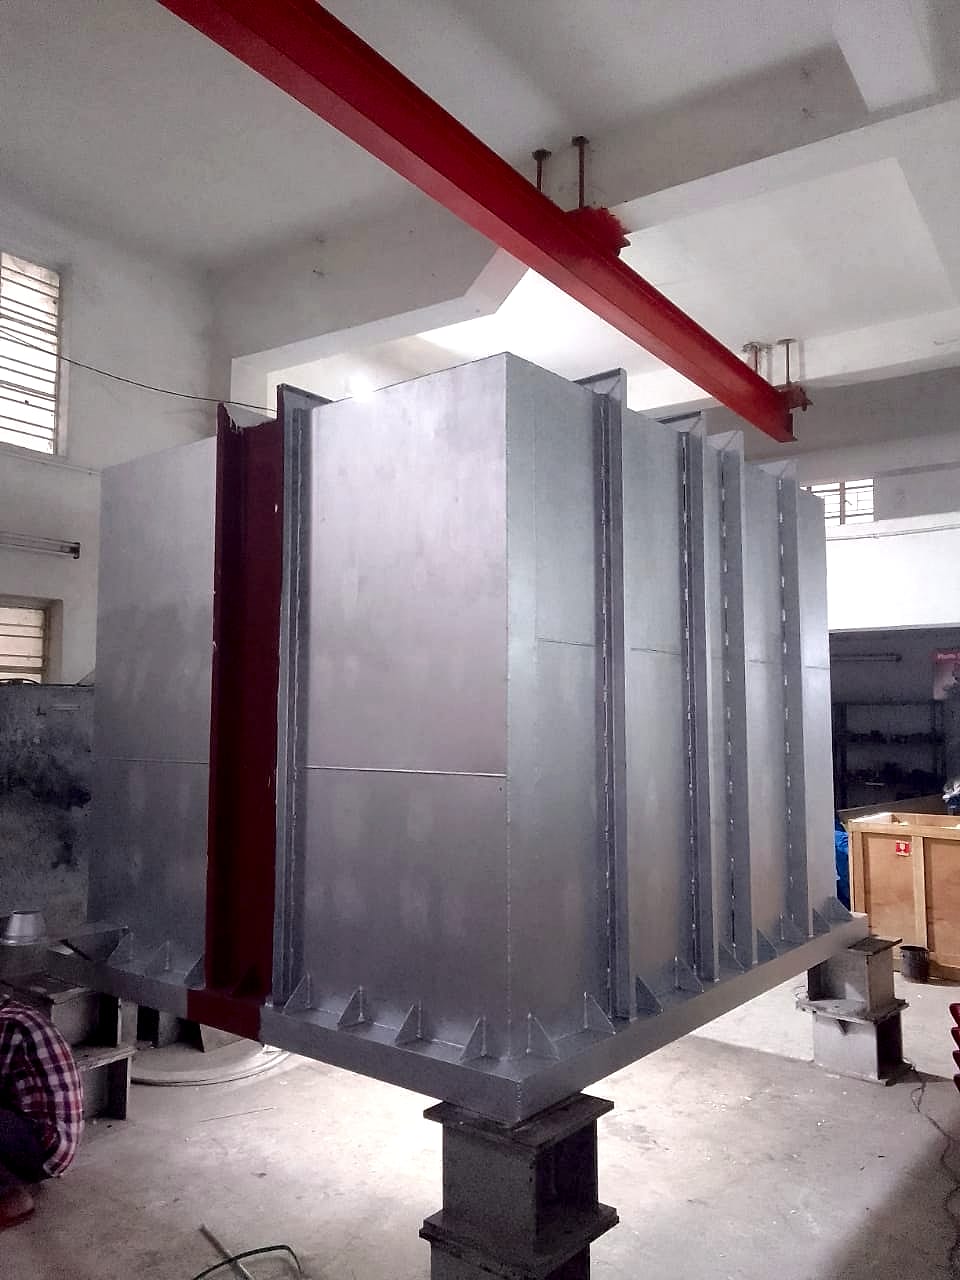
A new bell-type annealing furnace for cast iron
A new 60 kW bell-type annealing furnace for cast iron: a Fibrothal heating system, two heating zones and a PLC control panel with SCADA, running at 950 °C.
- Capacity
- 2 MT
- Rated power
- 60 kW
 Revamp
Rotary hearth furnace
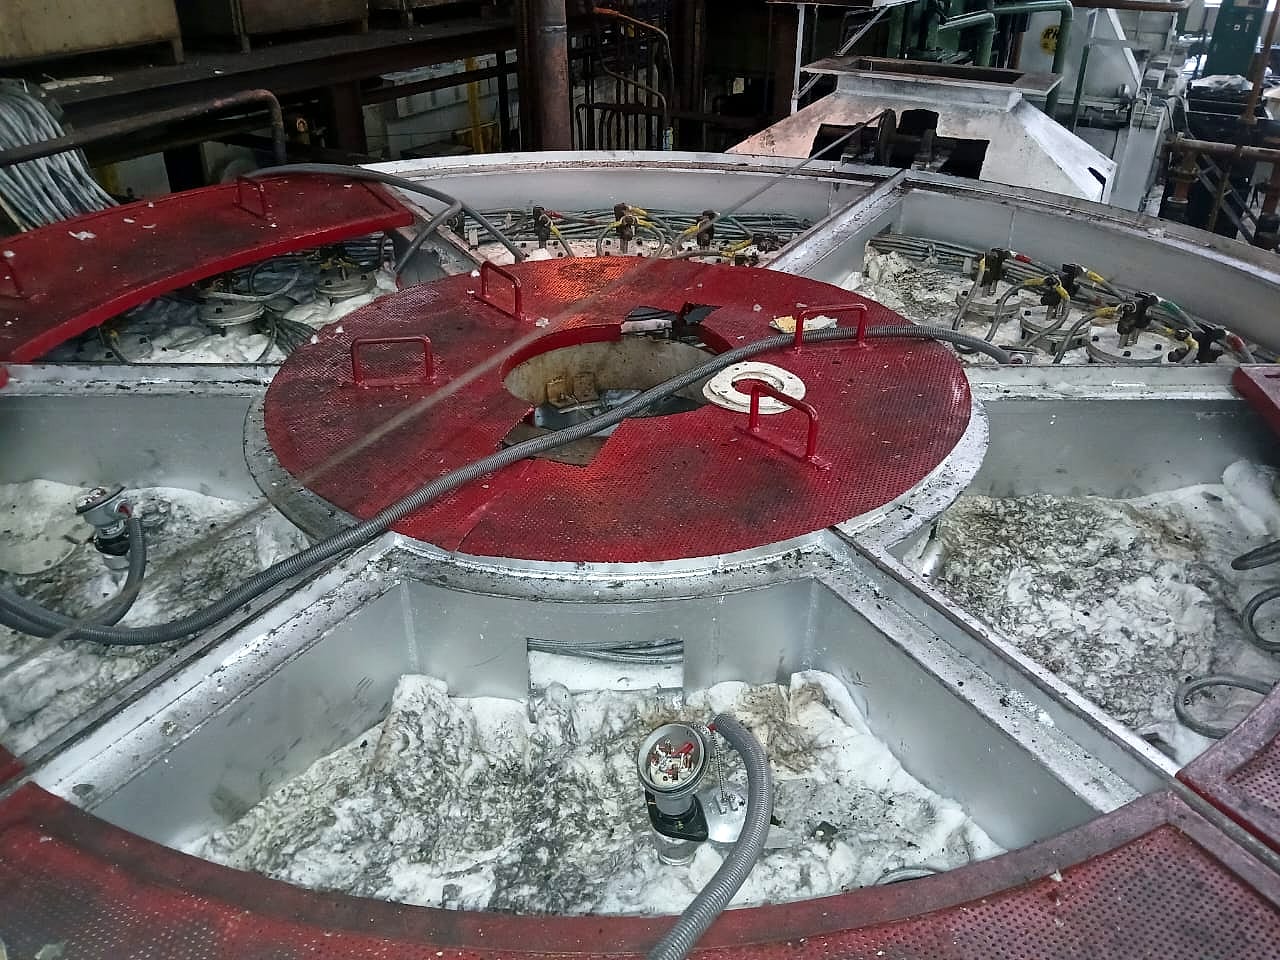
Revamping a rotary hearth furnace that kept failing
A bearing manufacturer's rotary hearth furnace kept losing element connections and hood insulation. We redesigned the elements and their cold zone, and relined the hood with high-temperature ceramic board.
- Charge weight
- 300 kg
- Rated power
- 180 kW
 Retrofit
Aluminium holding furnace
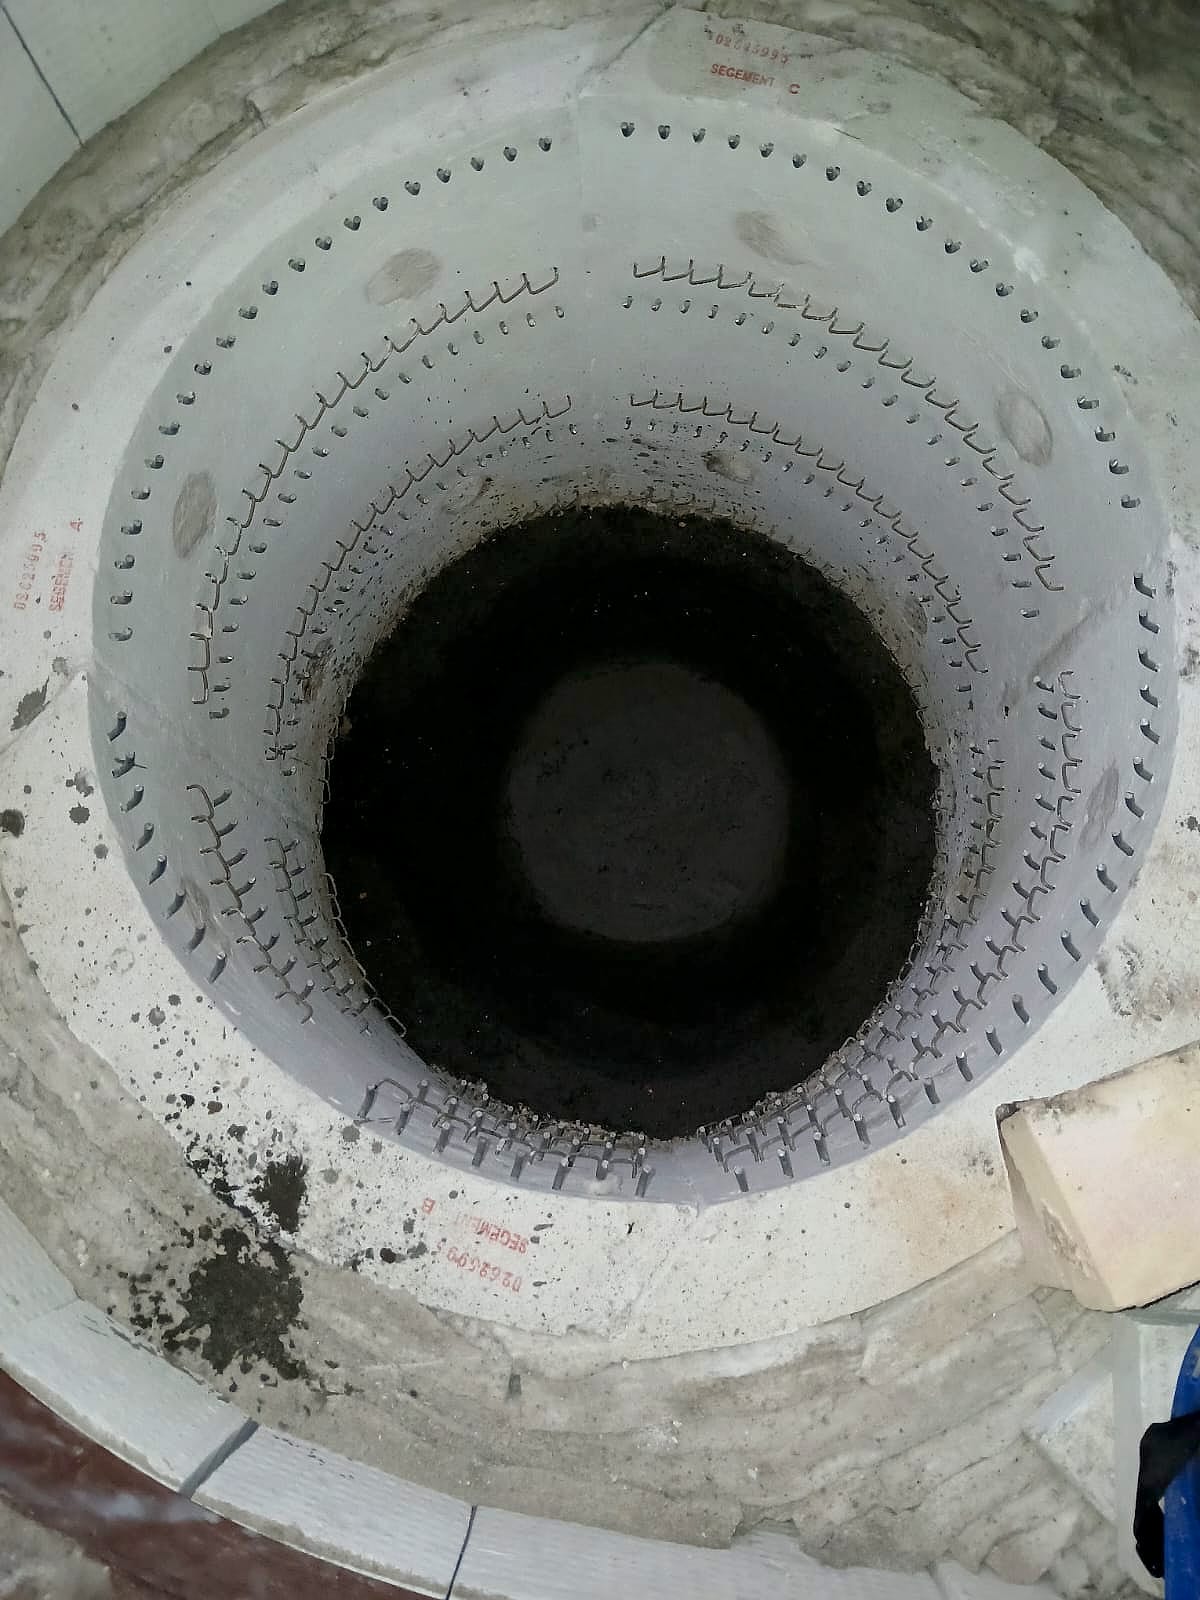
Revamping of Aluminium holding furnace
An aluminium holding furnace where every crucible failure took the SS310 heating elements down with it, for 15 days at a time. We rebuilt it with a Fibrothal heating system and Kanthal AF elements at line voltage, and a crucible problem now costs about 2 days.
- To recover from a crucible failure
- 15 → 2 days
- Charge capacity
- 300 kg/h
Start a project
Have a project in mind?
Share your load, temperature and cycle time. Our engineering team will reply within two business days.
We reply within two business days.